Address
Caochang Industrial Area, Liguang Rd, Lishui, Nanhai, Foshan, Guangdong, China
Phone:
0086-20-8938 9313
0086-757-8938 9313
Email:
Work Hours
Monday to Friday: 8AM - 10PM
24x7 online service
Address
Caochang Industrial Area, Liguang Rd, Lishui, Nanhai, Foshan, Guangdong, China
Phone:
0086-20-8938 9313
0086-757-8938 9313
Email:
Work Hours
Monday to Friday: 8AM - 10PM
24x7 online service
Custom LED Light Box & SEG Display Manufacturer
Approve a powder-coated poster stand with an identified finish reference, recorded surface checks and evidence for the coating properties your project needs.
For retail fixture purchasers and signage distributors, the useful outcome is a finished sample that can be compared, assembled and received against a clear agreement. Color, texture, marks at joints and packing protection need their own checks. Keep appearance approval separate from any requested coating test, and record which actual stand and production finish each piece of evidence represents.
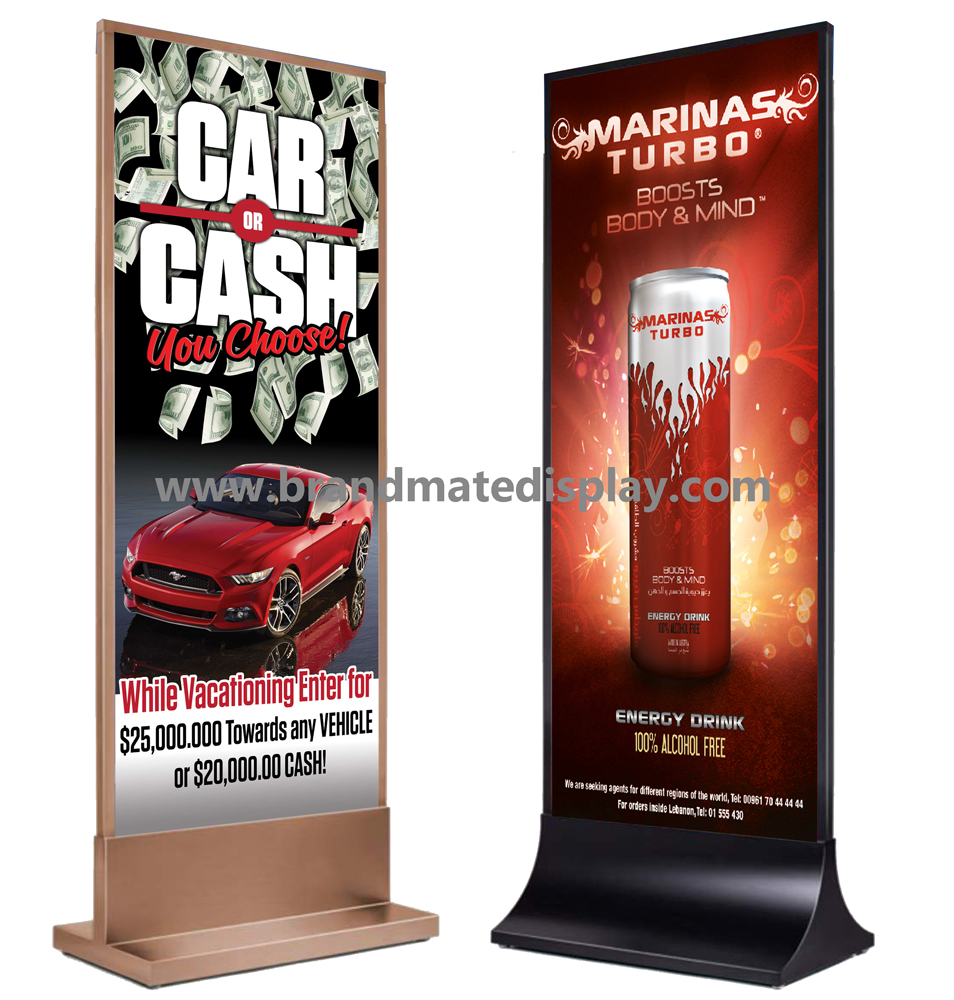
The photograph shows two upright framed poster displays with different visible frame and base finishes. Use the BrandMate Stand Display family as a starting point for the product discussion. Confirm the selected stand’s actual metal and coating system through its specification and sample; the image does not establish either.
Identify the proposed stand model, component drawing revision, base metal and coating system before requesting a finish approval. Ask BrandMate to confirm the actual preparation and finishing route for that proposal. A dark or metallic-looking frame in a photograph does not identify its substrate, powder formulation, pretreatment or cure. Keep those details open until the selected configuration has supporting information.
Agree a physical coated reference for color, sheen and texture. A color code helps identify the intention, but the approved reference should also show the surface character you want: smooth, textured or another defined appearance. A small flat swatch can help with color comparison; include a representative finished corner or component when the stand’s bends, joins and edges matter to approval.
Record the lighting, viewing distance, orientation and customer-visible surfaces used for the visual decision. Compare the reference and sample side by side under those agreed conditions. Use close views or light from an angle to locate a mark, then judge its cosmetic acceptability under the agreed viewing conditions. This keeps a diagnostic photograph from silently becoming a different inspection rule. Photographs help locate differences; they cannot reproduce a physical finish reference reliably on every screen.
Name the buyer or finish reviewer who can accept the reference and any permitted variation. Retain the sample ID, finish reference and approval date together. If the proposed texture or sheen differs from the reference, request a specific alternative sample and written decision before approving that change for quantity production.
Map the front, rear, sides, base and normally concealed contact areas on a drawing or annotated sample photo. Agree which areas are visible in the intended installation and which become visible during normal servicing. Use the same map for sample and receiving checks so a concealed fastener face is not confused with the front of a retail frame.
Examine the identified surfaces without scraping them or running fingers along uncertain cut edges. Look for differences in color and sheen, unwanted texture, embedded particles, pinholes, scratches, chips and areas that appear uncovered. Texture may be intentional; compare it with the agreed reference before describing it as orange peel or another defect. Record the location and visible appearance without guessing the process cause.
Pay particular attention to cut edges, bends, weld transitions, screw seats and the junction between upright and base. Ask whether any exposed area is an intentional masking or mating feature on the drawing. An unexplained uncovered edge needs review; additional coating must not be assumed to solve a fit, preparation or geometry issue. Keep a clear overview and a close image with a size reference beside the mark, without attaching anything that could alter the finish.
| Area | Compare or observe | Retain | If outside the agreement |
|---|---|---|---|
| Customer-visible frame and base | Color, sheen, texture and marks against the physical reference under agreed conditions. | Reference ID, surface map, conditions and overview/detail photos. | Identify the affected surface and request a corrected sample or explicit variation decision. |
| Edges, bends and weld transitions | Visible coverage, chips, pinholes or unwanted build-up; distinguish intentional masked features. | Drawing location and close image showing the extent of the observation. | Request review of the actual feature and repeat its check after correction. |
| Fastener seats and mating faces | Intended seating and visible finish condition before and after instructed assembly. | Matched before/after views and the component/fastener revision. | Review the fit and contact arrangement before accepting another finish sample. |
| Normally concealed areas | The separately agreed appearance and functional requirements for those locations. | Zone definition and any approved exception tied to the drawing. | Resolve the exception explicitly; do not extend it to visible surfaces. |
Photograph the sample before assembly, including the underside of the base and the parts that contact each other. Have the intended operator follow the supplied instructions with the specified hardware and tools. Review tightening requirements with the maker; do not invent torque values, force a coated thread or modify a mating part to make the sample fit.
Check the normal contact between upright and base, screw heads or washers, brackets and any moving or removable parts included in the quoted design. Observe whether parts seat correctly and whether instructed assembly creates a scratch, chip, loose coating or unwanted rubbing. Repeated assembly is a separate trial: agree its sequence and number of cycles before testing, using a representative sample designated for that purpose.
Take matched views after the agreed sequence and identify the first step at which a change appeared. Preserve the actual fastener, washer, spacer or contact detail in the record. If a part binds or coating is displaced, stop that step and request a reviewed correction. Recheck the affected fit and finish together after the correction rather than accepting a cosmetic touch-up as proof that the contact problem is resolved.
This check establishes what happened during the recorded handling sequence. It does not produce a universal scratch rating or establish stability, load capacity or outdoor suitability. Those functions require their own configuration and acceptance review. Keep the finish sign-off tied to the actual sample and agreed use.
Translate a requirement such as scratch resistance into the actual concern: adhesion to the substrate, film hardness, repeated abrasion, or damage at a particular assembled contact. These are different questions. A coin, key or fingernail demonstration has uncontrolled tool shape and force, so it is not a substitute for an agreed test method and acceptance criterion.
Where objective evidence is needed, ask the responsible technical reviewer or test provider to select an applicable method and edition. Agree the specimen, substrate, preparation, coating system, conditioning, relevant equipment settings, sampling and acceptance limits before the test. Record whether a flat test panel or an actual stand component will be used, and how it represents the proposed production finish. A panel result does not by itself settle coverage or contact damage at a shaped stand joint.
| Question | Evidence to specify | Report details to agree | Boundary |
|---|---|---|---|
| Does the coating remain attached? | An applicable adhesion test on an identified coating/substrate system. | Method/edition, specimen, preparation, rating criterion and observed failure location where relevant. | A tape-test rating is not an absolute bond-strength measurement or a service-life prediction. |
| How does the film respond to a hardness check? | An applicable film-hardness method, such as an agreed pencil test. | Specimen, method, identified test materials, endpoint and acceptance criterion. | A hardness result is not an abrasion result or a promise that normal handling cannot mark the stand. |
| How does the finish respond to repeated wear? | An applicable abrasion method on a suitable representative specimen. | Method, contact/abrasive system, load, cycles, result measure and acceptance limit. | Controlled wear on a flat panel does not reproduce every edge, fastener or transport contact. |
| Is the film within the specified thickness range? | A suitable dry-film thickness measurement plan for the actual coating and substrate. | Instrument suitability and verification, locations, readings, units and agreed range. | Thickness readings alone do not establish adhesion, hardness, coverage at every edge or corrosion performance. |
Have trained personnel perform any cutting, abrasion or other damaging test on designated specimens under an agreed plan. Do not experiment on finished stock or an assembled stand in service. Keep the signed appearance reference available separately from a specimen altered by testing.
Request a report that identifies the model or specimen, revision, date, method, conditions, sample count, measured result and responsible tester. If the specimen differs from the quoted product, obtain a technical explanation of what the result can support and what still needs checking. Outdoor exposure, cleaning chemicals or corrosion requirements need separately relevant evidence; no hardness, adhesion or thickness result establishes them automatically. BrandMate test availability, measured ratings and acceptance limits for your proposed finish require confirmation.
Obtain care instructions for the exact coating and any adjacent printed or clear surfaces. Identify the cleaners, cloths and handling routine intended at the site, then request confirmation of a compatible combination. Where a care trial is needed, agree it on a designated sample and compare the finish before and after under the same conditions. Record a change in color, sheen, texture or marks and request review; do not infer the cause from appearance alone.
Review the proposed packing with finished components in their intended carton positions. Identify where a base, upright, loose fastener or protective divider could contact a visible face. Ask for the proposed separation, corner protection, restraint and removal instructions to be shown on the sample packing plan. Protection must suit the actual finish and packing arrangement; an unspecified film or wrap is not evidence of compatibility.
Photograph the finished parts before packing and after the agreed unpacking or transport evaluation. If a mark is found, record its location alongside the matching contact point and the condition of the packaging. An intact carton alone does not identify when the mark occurred. Retain that evidence for review and recheck the revised packing where contact remains unresolved. An unboxing check is not a transport-performance certification.
Release the finish only against a record that identifies the approved sample, finish reference, stand/component revision, surface zones, visual criteria, assembly sequence, relevant test reports, packing revision and approver/date. State which checks passed, which exact variation was accepted and which items remain unresolved. A sample photo marked approved without those references can leave a replacement batch with no usable comparison.
For an observation outside the agreement, identify the affected part and request a proposed correction. Refinish, replacement and touch-up are different remedies; ask what is feasible and how the corrected part will be checked. A touch-up may differ in color, sheen or texture, so agree its visible acceptability and permitted locations instead of treating it as equivalent to the original finish. Commercial remedies and replacement availability require project agreement.
For quantity inspections, agree the lot definition, inspection sampling, decision criteria and handling of a nonconforming lot with the responsible quality team. Do not invent a universal allowable defect count. Keep the accepted reference and batch identification available for receiving checks. A change in substrate, preparation, coating system, component geometry or packing should trigger review of the affected approval evidence before it is carried over to a repeat order.
Use the BrandMate Quality Control and Warehouse & Logistics pages to frame the process discussion, then request the actual records and proposed provisions for your stand. General process information does not establish a particular finish rating or packing result.
Send BrandMate the stand drawing or reference, intended environment, physical finish reference, customer-visible surfaces, contact/changeover routine, cleaning requirements, quantity and destination. Identify any required coating tests and the decision they must support. Request the actual proposed material/coating details, sample plan, available evidence and packing arrangement. Exact specification, feasibility, sample cost, MOQ and lead time need project confirmation.
Compare the surface with the agreed finish reference and viewing conditions. A specified texture can be intentional; an unwanted difference still needs an identified location and decision. Record the observation and request review without diagnosing the coating process from a photograph.
No. Film hardness and the finish response at an assembled contact are different checks. Request an applicable hardness report if needed, and separately inspect the exact fastener arrangement before and after the agreed assembly sequence.
It can help establish color, sheen and texture. Include representative finished components for edges, bends, weld transitions and assembly contacts, then retain the complete sample record for quantity and repeat-order comparison.
Review the BrandMate Stand Display family and send the finish questions that need resolving for your selected configuration.
Tell BrandMate about the display and where it will be used. Share drawings and detailed specifications during the project discussion.